Industrial-Grade Prefab Accommodation Systems Engineered for Speed, Thermal Efficiency & Long Structural Lifespan
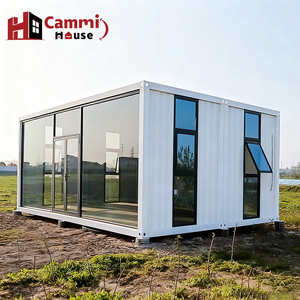
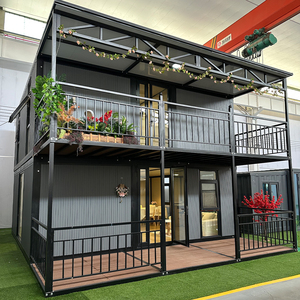
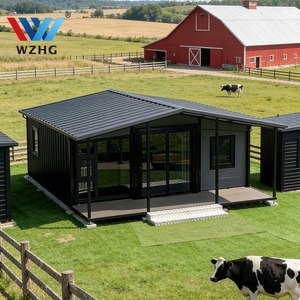
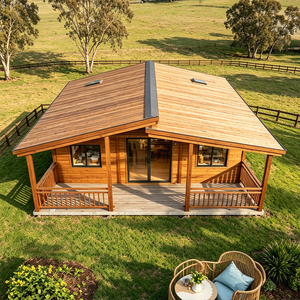
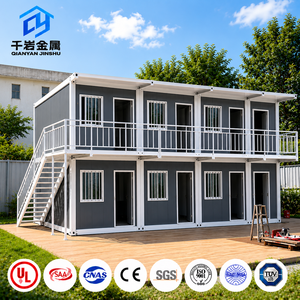
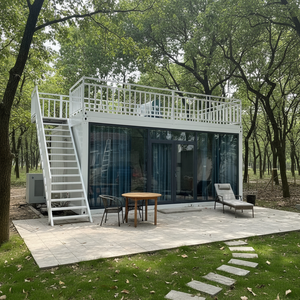
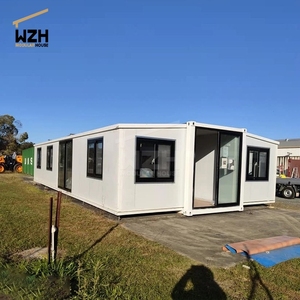
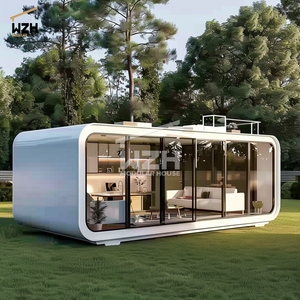
As international construction enterprises, mining conglomerates, and infrastructure developers expand global operations, the requirement for rapid-deployment, high-durability workforce housing has transitioned from simple temporary shelter to complex modular engineering. Selecting the China best prefab dormitory factory & supplier requires an extensive evaluation of structural framing integrity, thermal insulation physics, transport logistics efficiency, and compliance with international building codes.
Modern prefabricated dormitory systems manufactured in China leverage advanced cold-formed Q355B structural steel frames, hot-dip galvanization processes, and high-density thermal cores. By transitioning over 90% of construction tasks from unpredictable outdoor job sites to automated manufacturing facilities, modular construction eliminates site delays, reduces raw material waste by up to 60%, and ensures pinpoint quality control across multi-thousand-bed labor accommodation camps.
Standard commercial modular dormitory units utilize a self-supporting steel skeleton comprising cold-rolled corner columns, perimeter floor beams, and integrated ceiling trusses. Crucial structural parameters specified by top-tier Chinese manufacturers include:
• Primary Framing Steel Grade: Standard Q235B or high-tensile Q355B steel, treated with hot-dip galvanization ($\ge 180g/m^2$ zinc coating) to resist atmospheric corrosion in coastal and high-humidity environments.
• Enclosure Systems: Rockwool sandwich panels ($120kg/m^3$ core density) or Polyisocyanurate (PIR) panels engineered to deliver non-combustible Class A fire performance and thermal conductivity values down to $\lambda \le 0.022 W/m\cdot K$.
• Floor System Loading: Engineered floor frameworks supported by secondary purlins supporting marine plywood or fiber-cement boards, rated for live loads of $2.5 kN/m^2$ to accommodate multi-story bunk bed configurations.
To optimize procurement decisions based on site conditions, transport constraints, and assembly schedules, the following table compares key technical parameters across primary Chinese modular housing typologies:
| System Typology | Transport Shipping Ratio | On-Site Assembly Time | Wind Load / Seismic Rating | Thermal Core Options | Ideal Application |
|---|---|---|---|---|---|
| Flat-Pack Container Dormitory | 4 units packed into 1 SOC (20ft bundle) | 4 man-hours per 20ft module | 120 km/h wind / Seismic Zone 8 | 50-100mm Rockwool / EPS / PU | High-density labor camps, remote mining camps |
| Detachable Container Unit | Up to 8-10 units inside one 40HQ container | 6 man-hours per 20ft unit | 110 km/h wind / Seismic Zone 8 | 50-75mm Rockwool / Glasswool | Long-distance international sea freight export |
| Expandable Modular Cabin | 1 unit per 40HQ / 20ft transport chassis | 15 minutes deployment (2 workers) | 100 km/h wind / Seismic Zone 7 | 75mm Polyurethane (PIR) core | Emergency housing, rapid military mobilization |
| Heavy PEB Modular Steel Building | Packed as structural steel bundles | Phased construction schedule | Up to 180 km/h / Seismic Zone 9 | Insulated double-skin steel curtain wall | Permanent corporate housing, multi-story barracks |
Get direct factory pricing, structural calculation sheets, and 3D layout designs tailored to your workforce capacity.
Send an InquiryDelivering reliable modular accommodation requires seamless integration between automated factory production lines and on-site engineering execution. Operating under certified ISO9001 quality management frameworks and CE structural compliance (EN1090-1), our manufacturing facilities incorporate precision robotic welding, automated roll-forming machines, and strict material inspection protocols.
Precision structural steel welding on specialized assembly jigs guarantees absolute dimensional tolerance, ensuring perfect modular stacking up to 3 stories high.
Engineered with 4 internal corner downspouts integrated directly into the structural columns, eliminating exterior water staining and ponding risks during tropical downpours.
All electrical conduits, distribution boxes, LED luminaires, and sanitary piping are factory pre-installed to match localized international standards (CE, UL, SAA, SASO).
Specially engineered thermal break gaskets and high-density PU injection technology prevent thermal bridging in extreme climatic conditions from -40°C arctic cold to +55°C desert heat.
Flat-pack and detachable container designs are engineered around standard ISO shipping container dimensions, dramatically slashing ocean freight cost per square meter.
Units are fully equipped with modular sanitary pods, double-deck steel beds, ventilation systems, locker cabinets, and acoustic interior cladding panels.
The global modular construction landscape is experiencing a paradigm shift driven by stringent ESG (Environmental, Social, and Governance) standards, labor welfare compliance guidelines (such as IFC and ILO worker accommodation requirements), and rapid industrial automation. B2B buyers must anticipate several key structural shifts when specifying modular worker housing over the next decade:
Modern EPC contractors increasingly demand building components that support zero-landfill demolition policies. Prefabricated container dormitories function as 100% reusable physical assets. Upon completion of a major infrastructure or mining project, modular units can be dismantled, packed, and redeployed to a secondary job site up to 5 to 8 times without structural degradation. Furthermore, the structural steel components are 100% recyclable, drastically reducing the lifetime embodied carbon footprint compared to traditional masonry or timber barracks.
Energy consumption represents one of the highest operating expenses in large-scale remote camps. Next-generation prefabricated dormitories incorporate smart IoT energy management systems, including automatic occupancy sensors, smart HVAC thermostats, and solar-PV ready roof structures. Enhanced indoor air quality is maintained through continuous mechanical heat recovery ventilation (HRV) systems equipped with MERV-13 filtration, preventing humidity accumulation and mold growth in dense living quarters.
Worker retention and physical health are directly linked to accommodation quality. Modern modular dormitory layouts have evolved past bare minimum sleeping space to include optimized floorplan designs featuring dedicated laundry blocks, sound-insulated recreation suites, commercial kitchen/canteen modules, and private ensuite sanitary pods with anti-bacterial wall surfaces.
Understanding the technological trajectory of prefabricated housing provides crucial insights into why modern containerized modular systems have outpaced legacy site-built structures:
First Generation (Corrugated Sheet Sheds): Characterized by single-skin corrugated metal sheets with minimal structural steel, zero insulation, poor acoustic dampening, and extremely short operational lifespans under severe weather.
Second Generation (Standard K-Type / T-Type Prefab Houses): Introduced lightweight steel truss frames with thin EPS sandwich panels. While offering improved speed, K-type structures require high manual labor on site, offer limited wind resistance, and exhibit low durability against repeated dismantling.
Third Generation (Standard ISO Container Conversions): Utilized retired steel ocean freight shipping containers modified with cutouts. While offering robust shells, internal dimensions were heavily restricted, thermal bridging was difficult to resolve, and transport costs for empty hollow volumes were excessive.
Fourth Generation (Modern Modular Flat-Pack & Detachable Systems): The current industry standard perfected by top Chinese manufacturers. Featuring purpose-engineered steel corner castings, standardized structural frames, high-performance sandwich insulation, integrated roof drainage, and flat-packed logistics nesting, 4th-Gen dormitories deliver structural lifespans exceeding 20 years with rapid modular assembly.
Below are essential technical and logistical answers addressed by our engineering team to assist B2B procurement managers, contractors, and project planners:
A Flat-Pack container unit comes with a factory pre-assembled roof frame and floor frame; wall panels and corner columns are packed inside the frame sandwich. Four flat-pack units form an ISO-standard 20ft shipping bundle (SOC). A Detachable container house uses loose steel framing profiles bolted together on-site; because components are completely disassembled, up to 8 to 10 detachable units can be packed into a single 40HQ ocean container, drastically reducing ocean freight costs for long-distance transport.
Thermal performance is determined by sandwich panel core selection and thermal break engineering. For arctic climates down to -40°C, we specify 100mm Polyisocyanurate (PIR) or high-density Rockwool panels combined with double-glazed low-E vinyl windows and heated flooring substrates. For desert climates exceeding +50°C, reflective exterior steel coatings combined with continuous roof ventilation layers prevent solar heat gain.
Modular container dormitories distribute structural loads primarily through their four steel corner castings. Therefore, complete slab foundations are not strictly required. Units can be supported on concrete strip footings, localized concrete pier blocks, or heavy-duty steel screw piles placed directly beneath the corner posts, significantly minimizing civil foundation costs and site preparation schedules.
Our structural steel framework is non-combustible. The standard wall and roof enclosure panels utilize high-density Rockwool insulation rated as Class A non-combustible according to EN 13501-1 standards, capable of maintaining structural integrity under direct flame exposure for up to 120 minutes. All interior electrical cabling, junction boxes, and PVC conduit pipes conform to flame-retardant standards.
Yes. Standard 20ft and 40ft modular container housing units manufactured with 2.5mm–3.0mm structural steel corner columns are engineered to be safely stacked up to 3 stories high without requiring external structural steel scaffolding. External galvanized steel staircases, walkways, and balcony modules are bolted directly to the structural container frames.
With automated fabrication lines, standard factory production capacity ranges from 50 to 100 modular units per day. For a standard 500-bed camp project (approx. 100-150 container modules), factory manufacturing is completed within 15 to 20 days. Ocean freight delivery and custom clearance schedules vary depending on the destination port, while on-site assembly can be executed in less than 10 days by a crew of 12 workers.
Contact our structural engineering team today to receive CAD layout drawings, bill of quantities (BOQ), and factory-direct commercial quotations for your upcoming project.
Send an Inquiry